Secondary packaging · PE film bundle wrapping

Automatic PE Film Shrink Wrapping Machine Up to 25 Packs/Min.

PE Film Shrink Wrapping Machine lines peak at 25 packs/min on single-sheet PE film with 1-3 lane infeed, removable rack access, and PVC or POF on the checklist.

Up to 25 packs/minSingle-sheet PE film peak
1-3 lanesBottle infeed configuration

Get a Quote

Since 1995 · CE & ISO 9001 · 150+ countries

Shrink Wrap Line Capability Highlights

PE / PVC / POF FILM OPTIONSMULTI-LANE BOTTLE GROUPINGPLC + PNEUMATIC CYCLE CONTROLREMOVABLE FILM INJECTION ACCESSWATER · JUICE · CSD MULTI-PACKS
PLC-controlled sealing, cutting, and shrink cyclesPhotoelectric bottle detection and upstream pacing signalsInsulated shrink tunnel tuned for PE film bundlesProject FAT documentation and operator training packages
PE film bundle wrapping economics

Built for proven secondary packaging throughput.

Published marketing architecture positions this wrapper around grouped PET and glass bundles, highlighting faster cycles, lane-based infeed, and tunnel insulation that trims electrical demand versus conventional shrink lines—language mirrored here without inventing new mechanical claims.

Peak throughput
30Packs/min
Engineering ceiling with single-sheet PE film; lane count, bundle pattern, and resin choice can lower the observed rate.
Infeed flexibility
1-3Lanes
Matches the published “Bottle infeed on 1, 2 or 3 lanes” wording.
Automatic PE Film Shrink Wrapping Machine rated output equipment

Automatic PE Film Shrink Wrapping Machine — Up to 25 Packs/Min

Peak throughput
Up to 25 packs/min (single-sheet PE film)
Infeed configuration
Bottle infeed on 1, 2 or 3 lanes
Film handling
Film injection table on a removable rack for optimal access
Satisfaction Guaranteed
2 Years Quality Warranty
Overseas Engineer Support Available
On Time Delivery Guaranteed

Secondary packaging integration.

Bundle wrapping, lane-based metering, and tunnel shrinking are described on the original equipment page as a single automated loop for carbonated, water, and juice multi-packs, with an engineering ceiling of 25 packs/min on single-sheet PE film when bundle geometry and lane layout match the published checklist.

Lane-flexible infeed

1–3 lane bottle grouping keeps upstream conveyors balanced while the wrapper stages packs for film application.

PLC-driven sequencing

Photoelectric bottle checks, pneumatic push groups, and coordinated film feed mirror the published operating description.

Serviceable film deck

Removable film injection rack positioning is retained from the published marketing block to highlight maintenance access.

Operational Excellence.

UP TO 50%

Published advantage block cites faster wrapping cycles versus conventional bottle shrink systems.

UP TO 25%

Marketing copy on the published page attributes lower maintenance downtime to streamlined guarding and pneumatic logic.

UP TO 20%

Energy narrative references insulated tunnels and thinner film compatibility without altering published percentage claims.

The Core: Infeed. Control. Heat Tunnel.

Each step below reuses the photography and copy structure from the bundle shrink equipment page so art directors can trace imagery to its original slot.

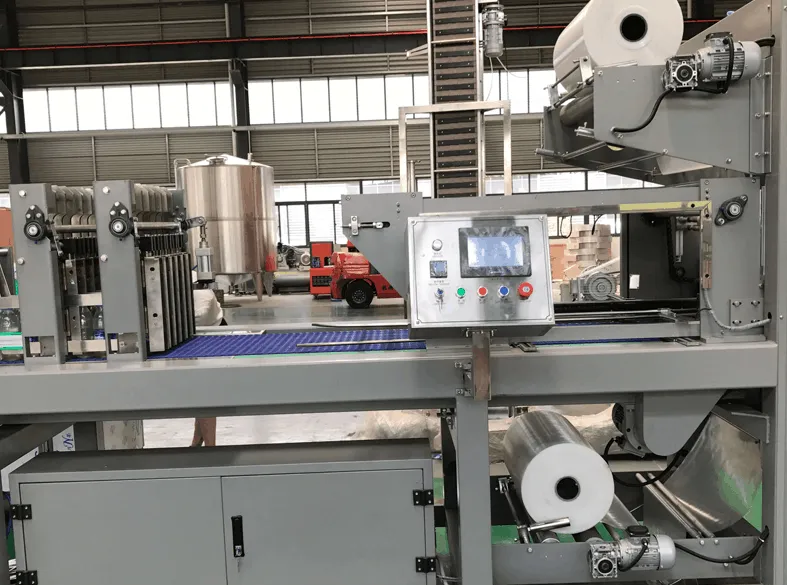
Automated bottle wrapping system with multiple infeed lanes

Multiple Infeed Lanes

  • Smart sensors meter bottles into one, two, or three wrapping lanes.
  • Lane layout stays synchronized with upstream Steplead PacTek filling modules per the published integration story.
  • Supports both single-bottle and grouped bundles before film enters the sealing station.
Automated bottle wrapping machine control panel

Intelligent Line Control

  • Tunnel infeed sensors detect missing bottles and throttle upstream conveyors.
  • PLC logic sequences push groups, film press, and cut cycles with operator overrides on the published touchscreen.
  • Signals can pause upstream equipment when multiple packs stack at the wrapper infeed.
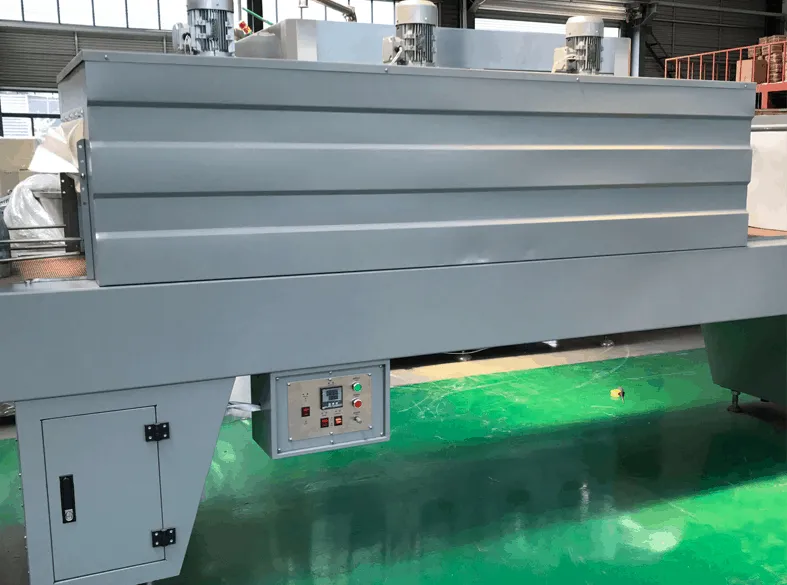
Bottle shrink wrap machine heat tunnel system

Heat Tunnel Efficiency

  • Insulated tunnel retains heat for consistent PE, PVC, or POF shrinking.
  • Marketing copy cites up to 30% lower energy draw versus conventional tunnels—restated here without new engineering numbers.
  • Cooling section after the tunnel stabilizes film before downstream conveyors.

Automatic PE Film Shrink Wrapping Machine Specifications.

Up to 25 Packs

Rated at up to 25 packs/min on single-sheet PE film — capture film mode, bundle count, and lane layout in RFQ acceptance notes.

Engineering Highlights

  • ControlPLC sequencing with pneumatic push, film press, and tunnel interlocks
  • SafetyDedicated emergency stop logic on the published operating description
  • FilmPE, PVC, and POF compatibility per on-page specification list
  • Quality systemsProject documentation can be aligned to ISO 9001:2015 quality management principles during factory acceptance.

Film thickness, tunnel temperatures, and electrical demand must be revalidated for every SKU mix. The ISO link explains the standard’s intent; it is not an on-page certificate claim.

Published checklist — bundle shrink wrapper

The public checklist under “PRODUCT SPECIFICATIONS of Bottle Wrapping Machines” lists film, tunnel, electrical, and envelope figures. Current engineering sign-off is up to 25 packs/min on single-sheet PE film with 1–3 lane infeed; confirm the rate against your FAT definition.

  • Packing material PE, PVC, and POF compatibility exactly as listed on the public checklist.

  • Film gauge window Film thickness: 0.03-0.15mm (verbatim from the published checklist).

  • Tunnel temperature band HeatingTemperature: Adjustable 160 - 260° (copied spelling and range from the checklist).

  • Power & footprint Power: 35kW. Dimension: 13,600 x 1,100 x 2,200MM (verbatim capitalization from the checklist).

ItemSpecification
Capacity headline (price table)Up to 25 Packs + Per Minute subline
Peak throughput (engineering)Up to 25 packs/min on single-sheet PE film
Packing materialPE, PVC, POF
Film thickness0.03-0.15mm
Heating temperatureAdjustable 160 - 260°
Electrical demand35kW
Machine dimensions (L×W×H)13,600 x 1,100 x 2,200MM

Layout collection & mechanical reference.

The “LAYOUT COLLECTION of Bottle Wrapping Machines” carousel on the original page still hosts two downloadable carbonated soft drink filling line PDFs (10,000 BPH and 2,000–3,000 BPH). They are retained here for buyers who need adjacent line-planning context next to the wrapper scope.

REF: SHRINK-MECH-SKETCH-2022
5 gallon filling line equipment layout reference with monoblock and process flow arrangement
Film & tunnel efficiency

Insulated tunnels and controlled film usage.

Energy narrative (on-page marketing)

Public copy describes tunnel insulation and thinner-film tolerance as levers for lower electrical draw versus conventional shrink lines—restated here without adding new engineering numbers.

Material fit

Checklist-level support for PE, PVC, and POF keeps procurement aligned with the film families already quoted on the public page.

Shrink wrapping line walkthrough.

“The bundle shrink stage gave us cleaner case presentation before palletizing. Film threading, tunnel curves, and conveyor spacing stayed aligned because the team treated commissioning like a packaging integration project, not a standalone machine drop.”
Packaging engineering lead — Still water & CSD co-packer, Southeast Asia
Exported to 150+ Countries24/7 Rapid Response SupportTurnkey Engineering Services

Get a Quote for This Machine

Since 1995 · CE & ISO 9001 · 150+ countries

FAQ — PE film shrink wrapping procurement

Which throughput numbers apply to our RFQ?
Engineering signs off up to 25 packs/min when the line runs single-sheet PE film with stable bundle geometry and the published 1–3 lane infeed. List your film mode, pack definition, and target cadence in RFQ so FAT matches the 25 packs/min ceiling.
Can we run PE, PVC, and POF interchangeably?
The public checklist lists PE, PVC, and POF as supported packing materials with a 0.03-0.15mm film window. Each resin behaves differently in the tunnel; expect trial wraps, seal bar tuning, and documented setpoints before locking a resin mix for production.
What utilities and envelope should we plan in MEP drawings?
The checklist cites 35kW electrical demand and overall dimensions of 13,600 x 1,100 x 2,200MM . Compressed air, conveyor interface heights, and operator walkways still need project-specific validation even when these baseline figures appear in bid documents.
How do we validate tunnel temperatures before startup?
The published module allows 160–260° adjustable heating (original spelling preserved in the checklist row above). Use that band as a starting conversation with iBottling engineers, then capture agreed setpoints, ramp profiles, and dwell time in the commissioning checklist—not just the headline numbers.
What lead time and documentation should we expect?
Request a milestone schedule that covers mechanical FAT, electrical drawings, and operator training packs. If you also need the adjacent CSD layouts, download the two PDFs in the layout section—the files keep the same URLs that were published on the original carousel.
Get A Custom Quote