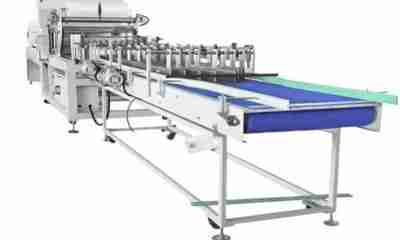
Sleeve register
Servo registration keeps the print seam and cut length aligned at the applicator.
Shrink sleeve labeling systems
Full-body sleeve labeling for bottles that need cut-length control, sleeve drop accuracy, seam orientation, and predictable shrink recovery through the tunnel and discharge zone.
Since 1995 · CE & ISO 9001 · 150+ countries
Built for beverage packaging project teams
A shrink sleeve line only performs well when sleeve roll registration, bottle spacing, cutter timing, applicator transfer, and heat-shrink recovery are engineered as one event. Listed performance is 9,000–21,000 bottles/h at 500ml, but the final guarantee is still resolved against bottle geometry, sleeve cut length, tunnel medium, and inspection scope before FAT.

 Bottle Sample FAT
 Label Roll Validation
 PLC/HMI Recipe Backup
 Commissioning Support Plan
The shrink sleeve platform is arranged around a longer chain than label-only systems: the sleeve must be cut correctly, dropped in register, carried into the shrink section, and leave the tunnel without twist or graphic distortion.
Sleeve feed, registration marks, and cut position stay readable before the applicator fires.
Spacing screws, guides, and transfer timing keep the sleeve centered as it drops onto the bottle.
Sleeve loading, tunnel adjustment, and change parts stay within the operator's working zone.
Sleeve register
Servo registration keeps the print seam and cut length aligned at the applicator.
Shrink recovery
Steam or electric heat settings recover the sleeve body without fish-eyes, wrinkles, or loose shoulders.
Changeover
Quick access to mandrels, cutters, and tunnel settings keeps bottle-family changes practical.
The sleeving sequence is engineered as one event: sleeve roll unwind, print-mark registration, bottle spacing, applicator timing, tunnel recovery, inspection access, and discharge flow are coordinated so the sleeve lands cleanly and the line keeps moving. That usually sits between a PET bottle blowing machine , a downstream coding checkpoint , and a bundle-wrap discharge stage .
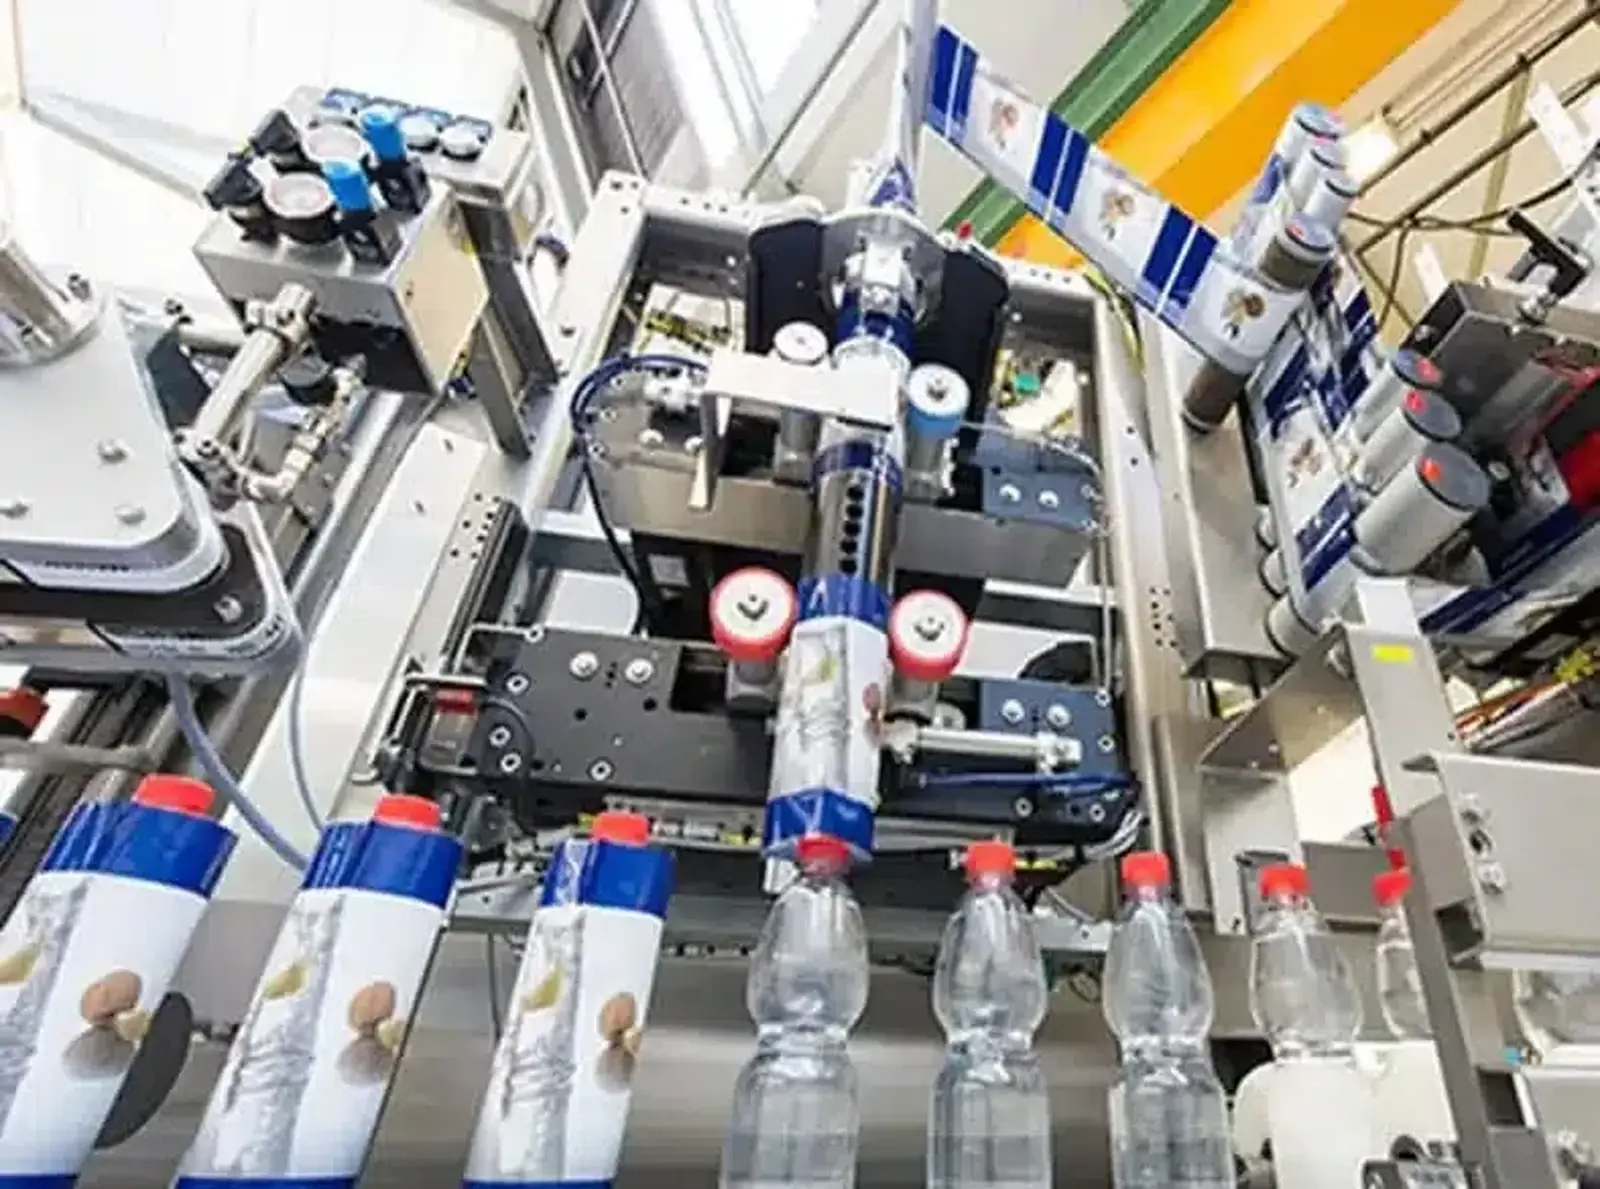
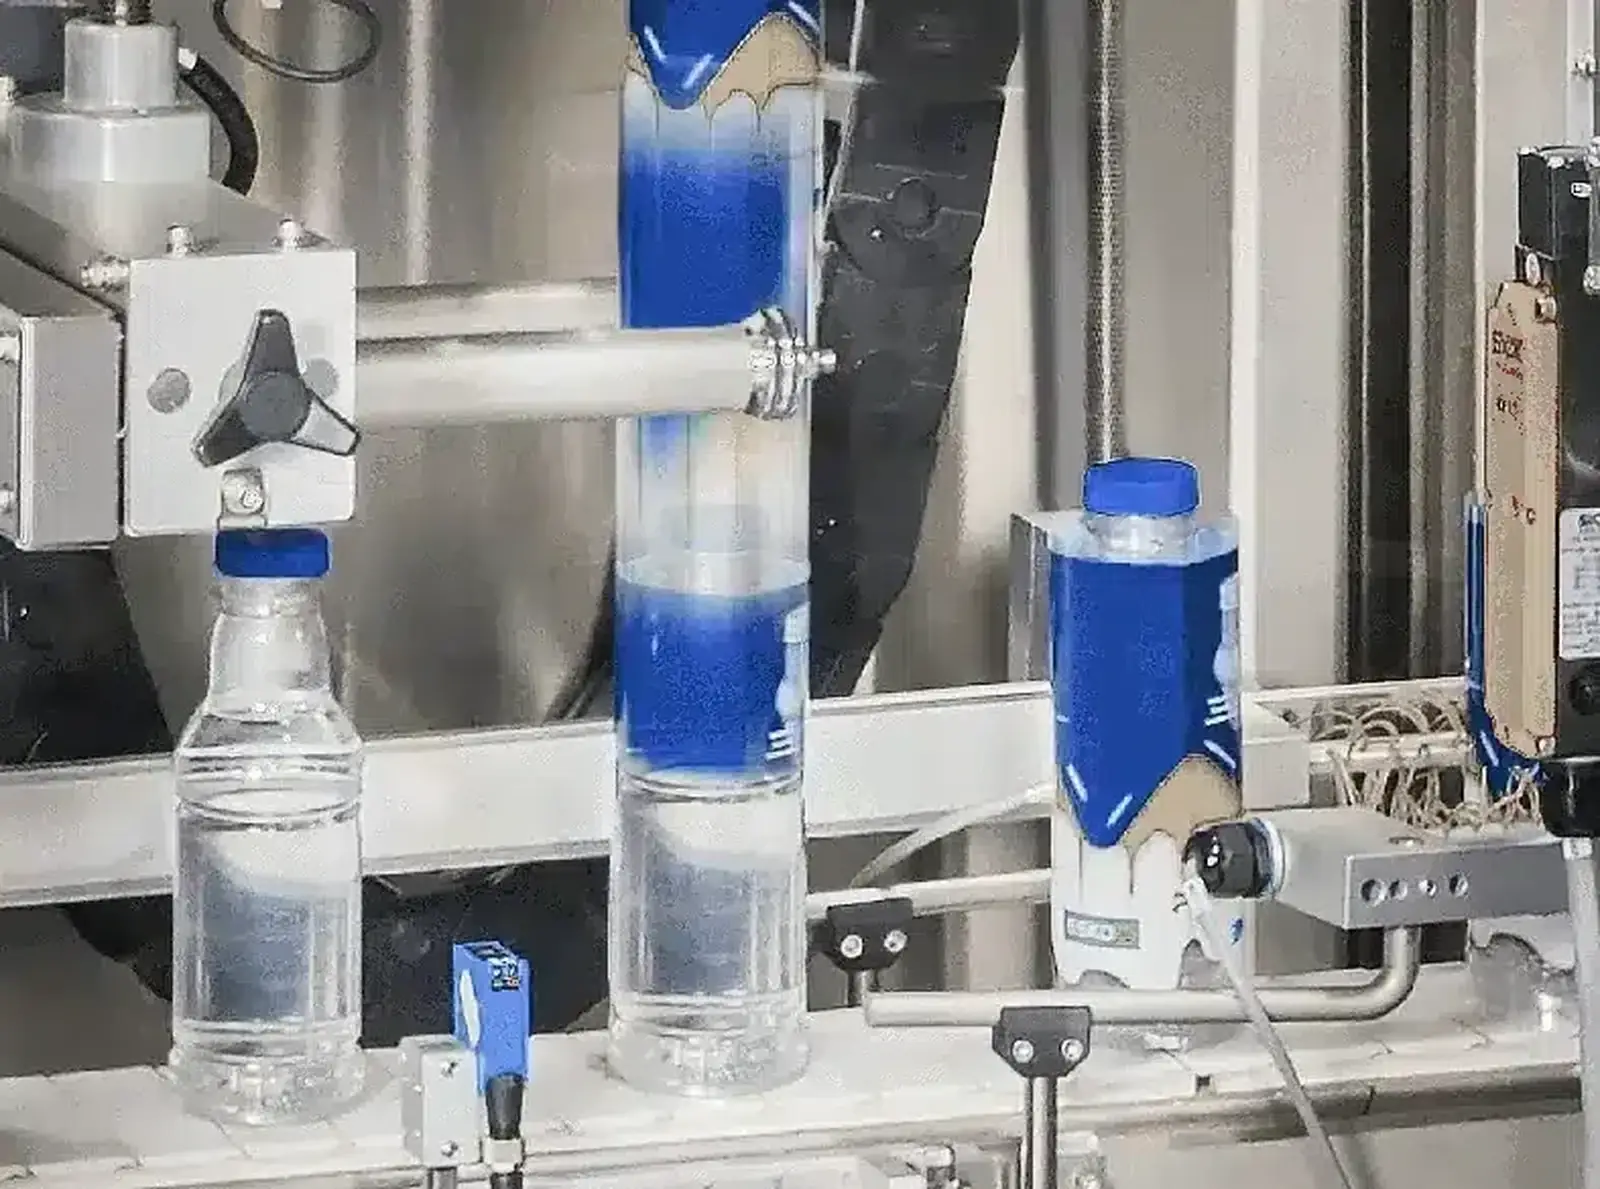
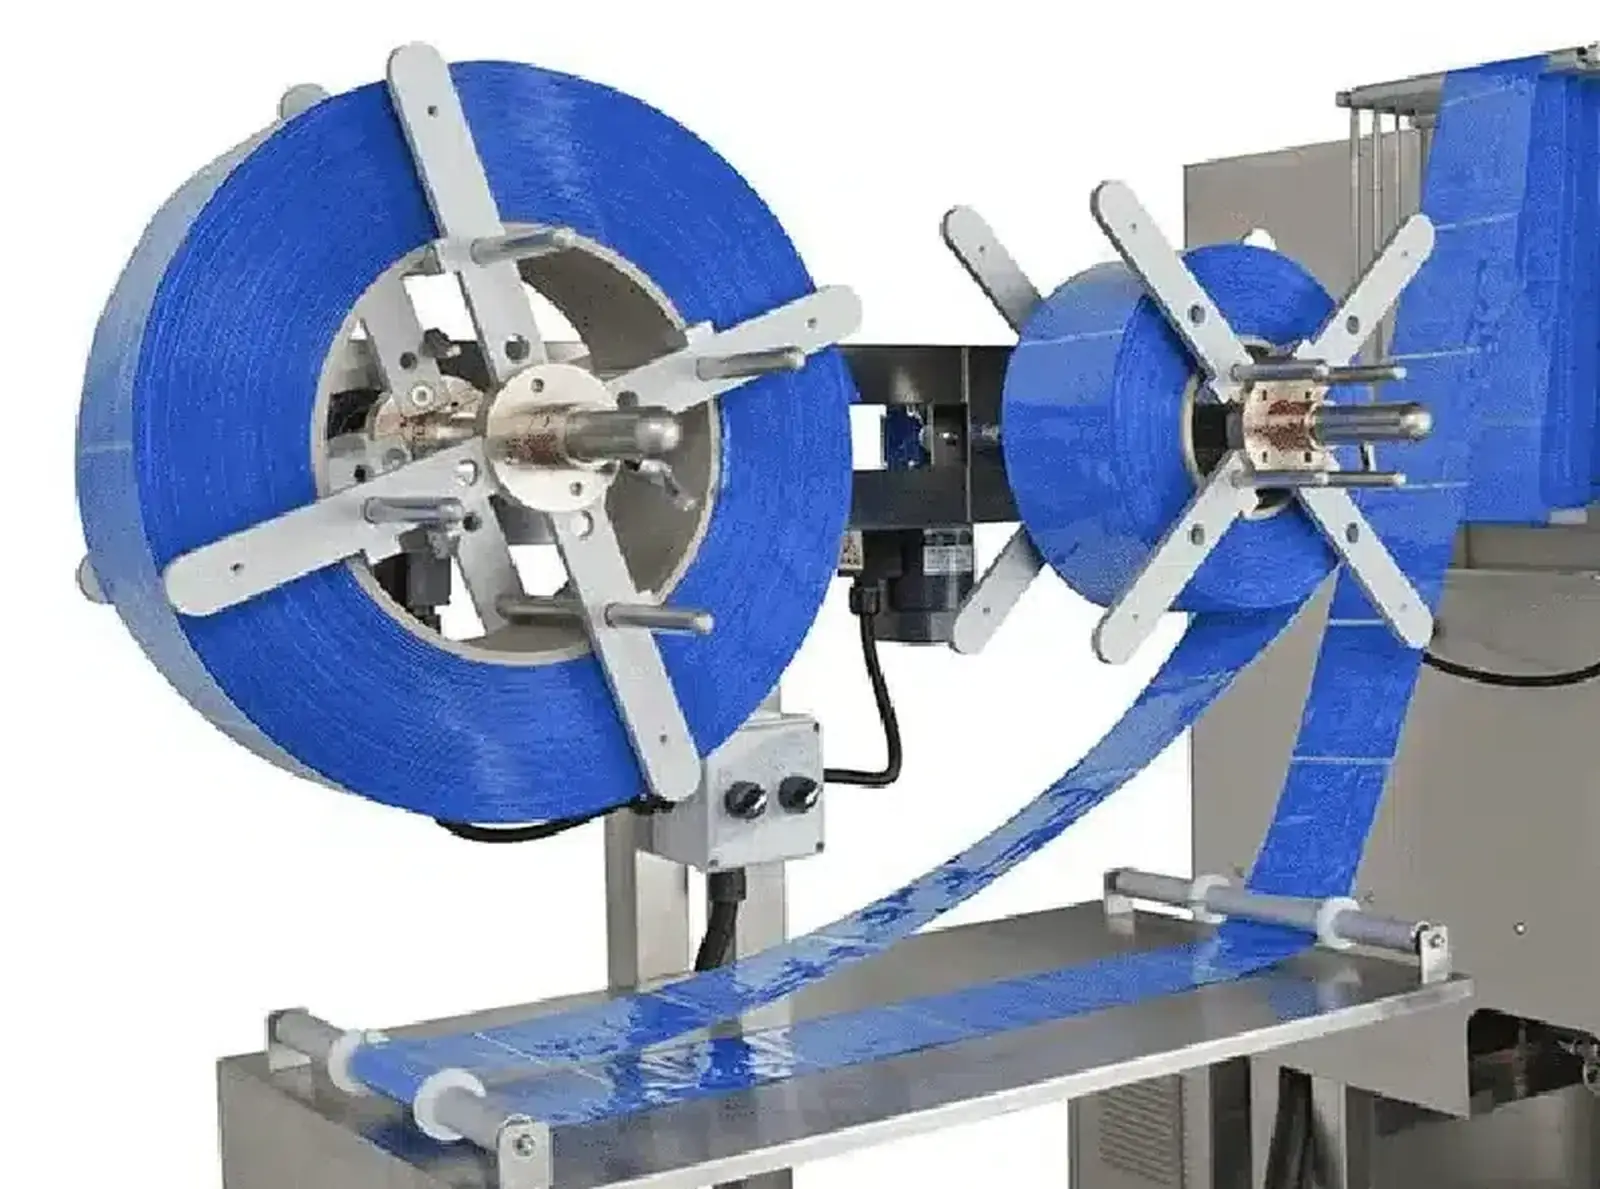
The quoted sleeve file set ties CE declarations, guarding notes, cut-length checks, tunnel-medium review, and bottle-sample acceptance records to the exact sleeve and shrink conditions tested during FAT, including the upstream bottle basis and the downstream traceability or wrap-pack interfaces locked in the project file.
Shrink sleeve projects depend on synchronized cut, drop, transfer, and shrink recovery, so the BOM names the PLC, knife control, applicator timing, tunnel hardware, conveyors, and reject interfaces that protect graphic alignment.
| Item | Specification |
|---|---|
| Model series | PET bottle shrink sleeve labeling platform |
| Output range | Rated at 9,000–21,000 bottles/h for 500ml; final guarantee tied to bottle handling, sleeve cut length, tunnel medium, and inspection scope |
| Container range | Round, square, and contoured PET bottles; diameter, shoulder shape, and shrink result confirmed by drawing and sample |
| Label dimensions | Sleeve layflat width, cut length, print-mark pitch, roll OD, and core size confirmed from sleeve-roll data sheet |
| Placement tolerance | Guaranteed only after FAT using production bottle samples, production sleeve rolls, and agreed inspection method |
| Label head | |
| Bottle handling | |
| Changeover | |
| Utilities and footprint | Power, air, tunnel medium, conveyor height, reel-loading clearance, and guard footprint confirmed on GA drawing |
These layout references reserve reel access, cutter service space, tunnel entry and exit clearance, heat or steam utility allowance, and downstream cooling distance before the GA drawing is approved.
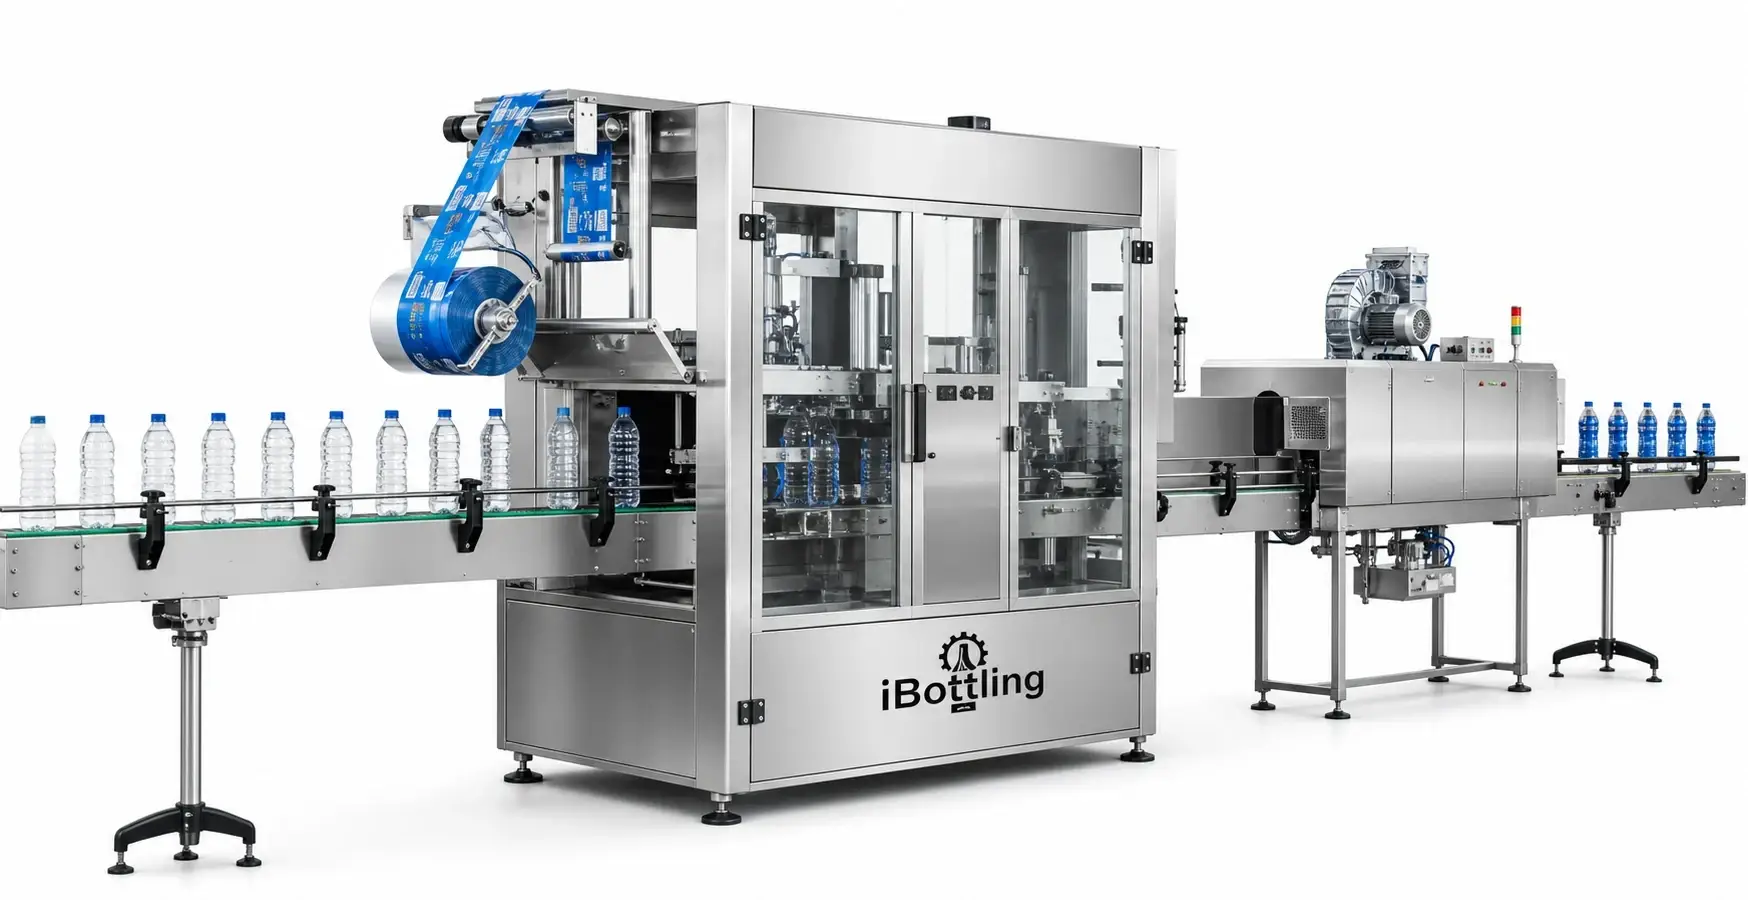
Controlled roll registration, cut-length accuracy, and tunnel recovery reduce seam offset, skewed graphics, and sleeve scrap.
Clear access to mandrels, cutter settings, and steam or electric tunnel recipes shortens recovery after bottle-family or sleeve-roll changeover.
Acceptance for shrink sleeve labeling should verify cut-length accuracy, sleeve drop timing, seam position after recovery, tunnel behavior, and clean restart after material and bottle changes.
Since 1995 · CE & ISO 9001 · 150+ countries

Complete beverage line engineering from treatment to packaging.
OEM-grade beverage lines — treatment, filling, blow molding, and packaging systems engineered for uptime, cleanability, and export commissioning.
HK: Chevalier House, 45-51 Chatham Road S.
Shanghai: Hope Business Bldg, No. 655, Fengzhou Rd.
Shenzhen: Overseas Friendship Bldg, No. 12 Yingchun Rd.
+86 (755) 8314-3479